Blog
March 20, 2015 | Company News
Neal Systems is pleased to announce the hiring of Steve Castino as part of our sales engineering team. Coming to us from GSI Instrumentation, Steve has 30 years of experience in the process industry and instrumentation fields with an emphasis in liquid and gas, process instrumentation, and control valves and actuation product lines for power, pulp and paper, chemical, pipeline, refinery, food and beverages, and education institution customers. He is customer-focused, a professional problem solver, and dedicated, making him a great fit for NSI and its customers. Steve will be assisting NSI Territory Manager Dexter Vilar with customer relationships in the greater New York City area and northern New Jersey.
March 20, 2015 | Company News
Neal Systems is proud to welcome Cass Janowski, formerly of ESC. Cass has spent the last 31 years with ESC servicing many of the water and wastewater municipalities in northern Jersey doing calibrations, installations, and repair of various types of instrumentation, controllers, and recorders. His specialties include flow measurement, replacing land-line modems with wireless systems, upgrades for PLC applications, and generally just finding ways to make the plants run when something isn’t working right. Somehow he became a Green Bay Packers fan in a world where the New York Jets and New York Giants reign supreme, but we don’t hold his cheeseheaded ways against him.
February 27, 2015 | Company News
NSI is pleased to announce that it has become a distributor of REGAL Gas Chlorinators. Used world-wide for municipal water treatment and wastewater treatment, REGAL products have a wide range of industrial, commercial, and agricultural applications, and allow the use of chlorine gas, which is the most economical method of disinfection, without sacrificing safety or reliability.
February 20, 2015 | Product News
Interested in the practical implications of the new ATEX Directive update 2014/34/EU? Click on the links below to download documents that will explain the changes. Make sure you’re ready before April 2016.
February 20, 2015 | Product News
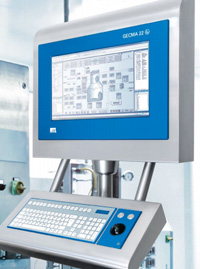
The GECMA RT is MTL’s new generation HMI series for safe operation in hazardous areas to reduce cost, maximize productivity, and increase plant safety.
The new GECMA RT is suitable for the strictest of hygienic conditions, aggressive production environments, and hazardous areas such as often found in the pharmaceutical, chemical, petrochemical, oil & gas and off-shore manufacturing industries. This future proof solution has been designed with state of the art technology and unique features to bring the best value:
- Unique and innovative platform concept. modular design saves time and cost during installation, commissioning; and operation
- Individually certified modules for quick and easy on-site maintenance
- 19″, 22″ Full HD and 24″ Full HD displays with LED backlight technology for optimum quality and viewing
- Lightweight, Slimline design helps to optimize space and offers flexibility of application
- Fiber optic or copper data transmission for cost effective, reliable, and increased volume of data transfer
- Unique Intrinsically Safe connection and Alarm visualization to ensure safe, continuous operation in the hazardous area
- Single line data transmission for simple, cost-effective installation and reliable transmission
DVI & USB interfaces/transparent USB for quick and flexible connectivity